
How To solve
common problems of preform products?
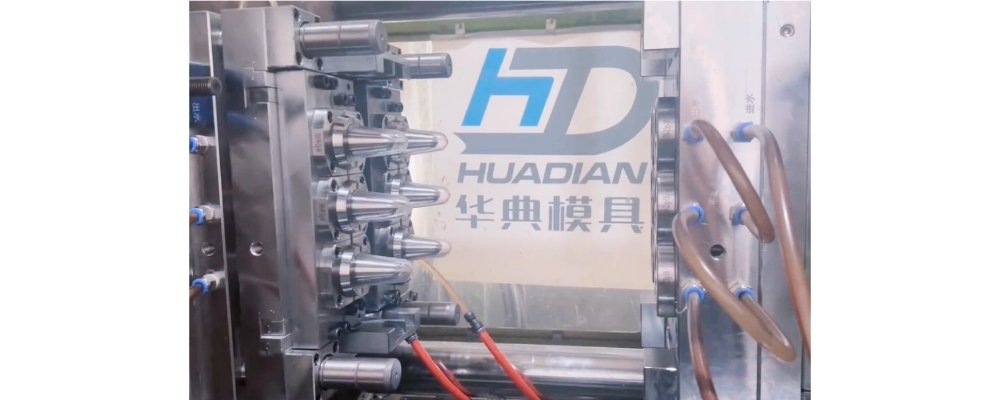
During the adjustment of preform mould, normally we will met some common problems of preform product, to obtain a high quality preform product, in addition to a good preform mold and a well-performing injection molding machine, the adjustment process is also extremely important.
As a professional preform mold manufacturer, we also possess certain experience in the adjustment process. The following are the common problems and solutions for preforms, providing some references for our customers who are following Huadian Mold.
Common problems and solutions for preform product
Preform Whitening
Whitening is usually caused by the following reasons:
A. The drying time is insufficient. Generally, the drying time should be 5 – 6 hours at a temperature of 170°C.
B. The temperature of the injection molding machine is low, and the material temperature is insufficient.
C. The temperature set in the temperature control box is not high enough.
D. Poor cooling effect.
Preform Silver Streaks
This situation occurs when the temperature is too high and needs to be reduced.
Preform Yellowing
A. The drying time is too long, and the material turns yellow.
B. The temperature of the hot runner is too high.
C. The copper nozzle or the heat insulation cap is damaged.
Preform Crystallization
A. The droplet-shaped crystallization is due to the injection time being too long or the injection pressure being too high, and it needs to be adjusted appropriately.
B. The bottom of the preform is too thin and requires an optimized design.
For more problems, feel free to discuss with us.
With over twenty years of professional preform mold manufacturing experience, if you have preform mold R&D and manufacturing requirements, please feel free to contact us.
Whatsapp: Ysaline+86 18367690166