
Ever ask yourself, Why do plastic parts keep warping, cracking or coming out wrong? This is a question that has been answered in the same way time and time again over my 9 years of experience working closely with PET injection molding machine lines.
Read this article to learn how viscosity, melt temperature, and back pressure impact the final product quality of your preforms. Find out which parameters to keep an eye on, how seemingly little adjustments may lead to major flaws, and which tests ensure that your output remains constant from shift to shift.
What Is PET Injection Molding And Why It Really Matters
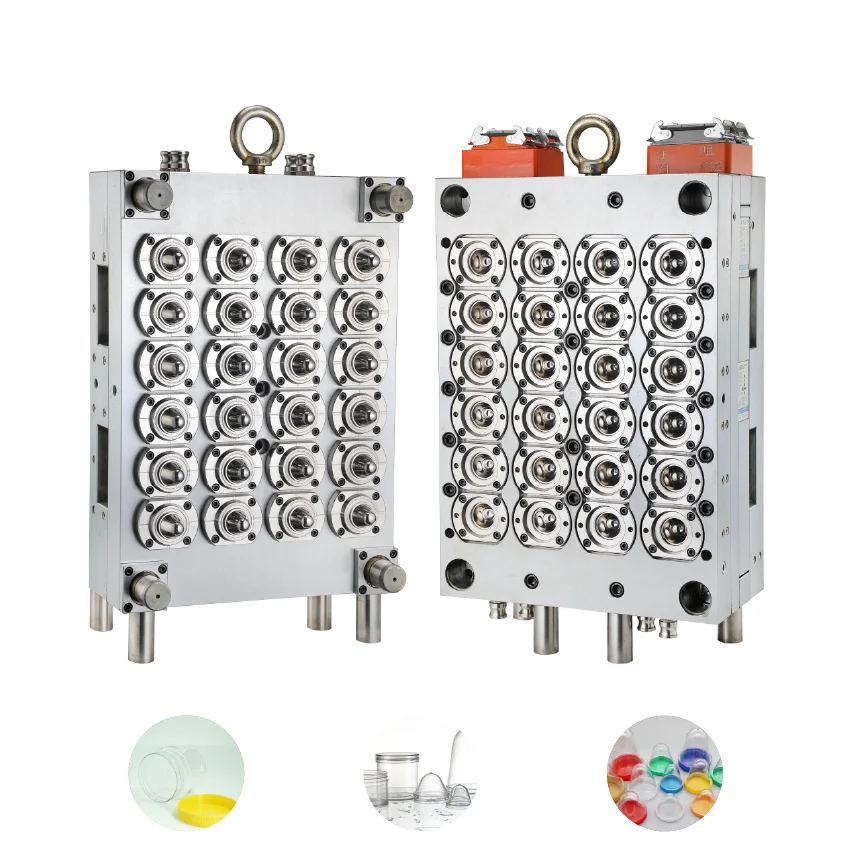
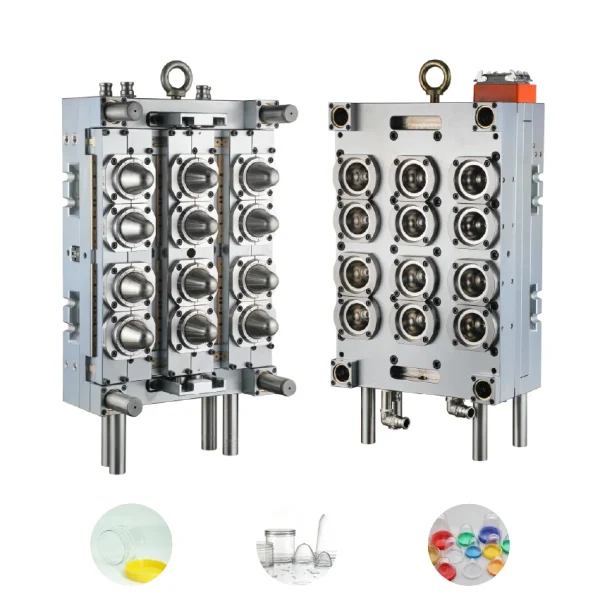
PET injection molding involves using a precise mould to shape melted PET plastic injection moulding resin into preforms. Bottles, jars, and other containers utilised in the food, drink, and cosmetics sectors are made from these preforms by reheating them and then blowing them into shape. A pet injection molding machine is essential to the procedure since it precisely heats, injects, and cools the plastic at each cycle. The success of each cycle is dependent on maintaining a constant melt temperature, a constant back pressure, and a constant resin viscosity.
A hazy, poor surface, uneven walls, or trapped bubbles could result from any of these things drifting in the preform. Since PET is both lightweight and sturdy, as well as completely recyclable, manufacturers depend on injection moulding PET technology. Less waste, cheaper production, and bottles that are perfectly clear and safe are the results of a well-executed procedure.
Core PET Molding Parameters At A Glance
| Parameter | Typical Range | Why It Matters |
| Melt Temperature | 270°C – 290°C | Controls flow, clarity, and gloss |
| Back Pressure | 5 – 15 bar | Affects melt mixing and weight |
| Drying Temperature | 160°C – 180°C | Removes moisture before melting |
| Injection Speed | Medium to fast | Prevents short shots and stress marks |
Why Does Melt Temperature Decide Preform Clarity?
When creating a temperature profile for pet injection molding, one of the first things I do is verify the melt temperature. The ideal melting point for PET resin is between 190 and 210 degrees Celsius, where it flows well yet does not degrade. If it’s too low, the preform will seem dull and will have noticeable flow lines all over it.
Resin becomes brittle, becomes yellow, or emits gases that alter the flavour of bottled beverages when the temperature is too high. Each performer maintains a consistent appearance and performance thanks to a uniform temperature profile throughout all heating zones.
Setting The Right Heating Zone Profile
In a typical PET preform machine, there are four or six heating zones distributed around the barrel, with the hopper being slightly colder and the nozzle being significantly hotter. The resin may melt uniformly without being shocked in any one spot thanks to its slow ascent.
Uneven melting and the potential trapping of unmelted pellets inside the shot are both caused by abrupt temperature swings across zones. The quickest and easiest approach to preserve resin quality throughout is to have a smooth, progressive contour.
Recommended Heating Zone Temperatures
| Zone | Temperature Range | Purpose | Risk If Wrong |
| Feed Zone | 250°C – 260°C | Initial softening | Pellets stick, feeding jams |
| Compression Zone | 265°C – 275°C | Even melting | Uneven melt, bubbles |
| Metering Zone | 275°C – 285°C | Final mixing | Color streaks, poor mix |
| Nozzle | 280°C – 290°C | Smooth injection flow | Stringing, drooling |
Quick Signs Your Melt Temperature Is Off
- The preforms seem murky or fuzzy close to the entrance.
- When ejected, a distinct plastic odour is noticeable.
- Transparent PET preforms take on a yellowish hue.
- Regular drooling or stringing around the tip of the nozzle
What Happens When Back Pressure Runs Too High Or Low?
Screw packing and mixing of molten resin before injection is controlled by back pressure. If you set it too low, the melt will remain loose and bubbles will form in the preform wall due to trapped air pockets. If it’s set too high, the pet injection molding temperature will rise over acceptable limits because of the additional shear heat, causing deterioration.
Without scorching the resin, the correct back pressure produces a thick and well-mixed melt. The standard operating pressure range for injection moulding machines used to make pet bottles is 5–15 bar, with small adjustments made for different grades of resin.
Finding The Balance Point For Back Pressure
It is common practice for operators to begin with a modest back pressure and gradually increase it, monitoring the preform’s weight and clarity along the way. Consistent shot weight, absence of bubbles, and smooth gate markings on every cycle indicate a good balancing point.
Back pressure is typically unstable if the weight continues to change between cycles. Adjusting this one parameter to perfection usually gets rid of issues that look like mould but are actually something else entirely.
Low vs High Back Pressure Compared
| Factor | Low Back Pressure | High Back Pressure |
| Melt Mixing | Poor, uneven color | Strong, uniform color |
| Bubble Risk | High | Low |
| Energy Use | Lower | Higher |
Energy savings from low back pressure come at the cost of increased bubble risk and shift-related weight oscillations. Although high back pressure enhances mixing, it stresses and shears the resin. For the majority of PET grades, the sweet spot is somewhere around the middle. You may discover the optimal ratio of resin to mould by doing incremental tests.
Advantages And Disadvantages of Watching
- Benefit: include enhanced colour and clarity even at moderate pressure.
- Benefit: consistent mixing results in fewer trapped bubbles.
- Drawback: resin temperature increases with excessive pressure.
- Drawback: differences in weight are caused by insufficient pressure.
How Does Resin Viscosity Affect Preform Wall Strength?
The viscosity of the molten resin indicates how readily it flows through the mold’s interior. The amount of recycling or reprocessing cycles, temperature, and moisture content all have an impact on the viscosity of PET resin. When using a high-viscosity resin in an injection moulding run for a pet preform, the injection pressure needs to be increased. It can make the walls thicker and more uneven.
Rapid flow is a benefit of low-viscosity resin, but uneven cooling could cause it to exhibit sink marks or short shots. Predictability of wall thickness and ultimate strength can be achieved by checking the inherent viscosity before each batch.
Why Drying Resin Before Molding Matters
Since PET resin is hygroscopic, it rapidly absorbs atmospheric moisture when exposed to it. Melting wet resin reduces its viscosity and weakens the final preform structure because it breaks down.
Before putting PET pellets into the injection moulding machine to make pet preforms, most factories let them dry for four to six hours at the right temperature. On a busy line, preforms that are brittle and weak are often the result of skipping this step.
Why Drying Resin Before Molding Matters
- Hand twisting preforms causes them to break quickly.
- Near the gate, sink marks are visible.
- The thickness of the walls varies among the cavities.
- With no modifications to the settings, the shot weight wanders.
Common Viscosity Problems And Quick Fixes
| Case | Problem | Likely Cause | Fix Applied |
| Case 1 | Brittle preform necks | Wet resin, low viscosity | Re-dried resin 5 hours |
| Case 2 | Sink marks at gate | Viscosity too low | Lowered melt temp slightly |
| Case 3 | Heavy, thick walls | Viscosity too high | Increased injection speed |
| Case 4 | Color streaks | High regrind ratio | Reduced regrind percentage |
As these examples demonstrate, issues with viscosity are typically caused by changes in temperature, humidity, or the resin mix ratio. To correct most faults without changing the whole recipe, small, focused tweaks are usually the way to go. One easy way to catch patterns early is to keep a basic diary of viscosity readings. Over time, this single behaviour avoids a plethora of expensive rejections.
Which Machine Features Protect PET Quality Long-Term?
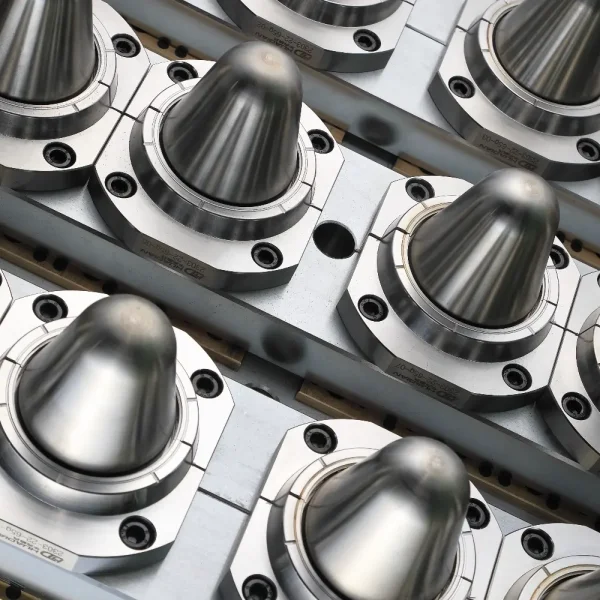
From the very beginning, quality control becomes much easier when you use the correct pet injection molding machine. Machines that have robust hydraulic or servo systems, precision screw designs, and closed-loop temperature control can maintain a constant melt temperature and back pressure cycle after cycle. Over time, a dependable pet injection molding machine will help save downtime and energy waste.
Because less expensive machines tend to wander out of setup more quickly, many customers weigh the cost of the pet preform injection moulding equipment against its reliability over the long run. In order to streamline the process of making both preforms and bottles, some lines additionally make use of a pet injection blow moulding machine.
Features Worth Checking Before You Buy
- Thermostatically controlled closed-loop barrel
- Pressure consistency achieved by servo-driven injection
- The hot runner pet injection mould is designed to be easy to clean.
- Operators’ real-time monitoring displays
- Questions and Answers Regarding PET Quality Control
Frequently Asked Questions
What Melt Temperature Is Best For PET Preforms?
Depending on the resin grade, the majority of PET preforms mould effectively within the temperature range of 270–290°C. Variables like as resin viscosity, mould size, and machine type determine the precise value. It is best to start close to the range indicated by the resin supplier and make incremental adjustments from there.
- Before anything else, verify the resin datasheet.
- Turn the heat up or down by 2 to 3 degrees Celsius.
- Be alert for changes in scent or colour.
For what reason are bubbles included within preforms?
Air bubbles, wet resin, or a back pressure setting that is too low for the resin grade are the most common causes of bubbles. Additionally, they may manifest if the resin’s melt temperature is insufficient to facilitate its smooth flow. In most cases, the issue goes away quickly after addressing one of these factors.
- Slightly raise the level of back pressure
- Allow resin to dry for a longer period of time before using
- Step-by-step increase the melt temperature
When should resin be allowed to dry before being moulded?
Each batch of PET resin should be air-dried for four to six hours at the recommended temperature. Bypassing this stage weakens preforms and decreases viscosity. As the resin batch ages and the humidity changes, the drying time could change marginally.
- Get a good dehumidifier.
- Make sure there is no excessive wetness.
- Get the resin re-dried if it becomes wet.
Why Is the Preform Wall Thickness Not Consistent?
Mould cooling unevenly across cavities, changes in viscosity, or an uneven melt temperature are common causes of uneven walls. You may discover this issue early by regularly monitoring the shot weight. A whole shift’s worth of little machine drift builds up fast.
- Every hour, record the shot weight.
- Make that the cooling channel flow rates are being monitored.
- Regularly re-adjust temperature sensors
Conclusion
Most problems may be fixed with little tweaks rather than a complete system overhaul. If you are looking to update or are in need of a reliable PET injection molding machine that can handle this degree of control, Huadian Mould Co., Ltd. provides proven equipment, transparent technical assistance, and affordable solutions for purchasers of all sizes.
Working with a manufacturer who has a firm grasp on these three areas will lead to improved bottles, less rejections, and a more streamlined manufacturing process overall.